
Automotive components
Automotive parts cleaning, South America
An automotive component supplier in South America produces brackets, stampings and suspension parts for an e-coating line. The parts arrive with stamping scale and light rust, and the plant previously cleaned them in batches. Flat brackets nested in the batch, so some faces were shielded and others were marked by contact. The coating line needs a consistent surface on every part, and the supplier wanted a continuous process that could run at the line takt rather than a batch cycle. The supplier runs several part families on the same line, and the cleaning step has to change over without stopping the e-coat line for long.
A QWD800 mesh belt shot blasting machine was chosen for continuous handling. The through opening is 800 × 500 mm and the conveying speed range is 0.5–4 m/min, which suits the bracket sizes and the line rhythm. Published throughput is 1.0–3.0 t/h, and the line runs at 2.4 t/h. Parts are spread on the mesh belt and pass through the blast zone without fixtures, then discharge onto the existing conveyor. The machine was placed between the press cell and the e-coat loading station. The mesh belt was selected over a roller conveyor because small brackets would fall between rollers, and the belt width and opening were checked against the widest suspension bracket. The machine footprint allowed the existing fork-lift route to stay open.
The belt speed is set at 1.8 m/min for the current mix. Parts are loaded in a single layer so each face sees the blast stream, and the review identified a small group of parts that need a second pass because of their shape. The dust collector is rated at 12000 m³/h and is connected to the belt chamber, and the abrasive recovery system returns shot after separating dust and fines. The operator checks the belt loading and the discharge before each shift. The loading crew uses a simple gauge at the entry to keep parts inside the opening, and the exit chute was adjusted so parts do not drop onto each other. The blast wheels are checked for blade wear every maintenance window, and the mesh belt is inspected for tracking and tears.
At 2.4 t/h the line keeps pace with the press cell and the e-coat line without building a buffer. The supplier checks a reference bracket for surface and profile at the start of each run. The continuous flow removed the nesting problem, and the flat faces now reach the coating stage without contact marks. Delivery included the belt foundation, the interface with the existing conveyors, commissioning on production parts and operator training. Wear parts and belt tracking are included in the preventive maintenance plan. Changeover between part families is handled by the recipe list, and the first parts of a new run are checked before the line speed is released. The supplier also keeps a spare mesh belt on site because a torn belt would stop the line. The installation was commissioned during a planned shutdown so production restarted on schedule, and operators were trained on belt loading, emergency stops and daily checks.
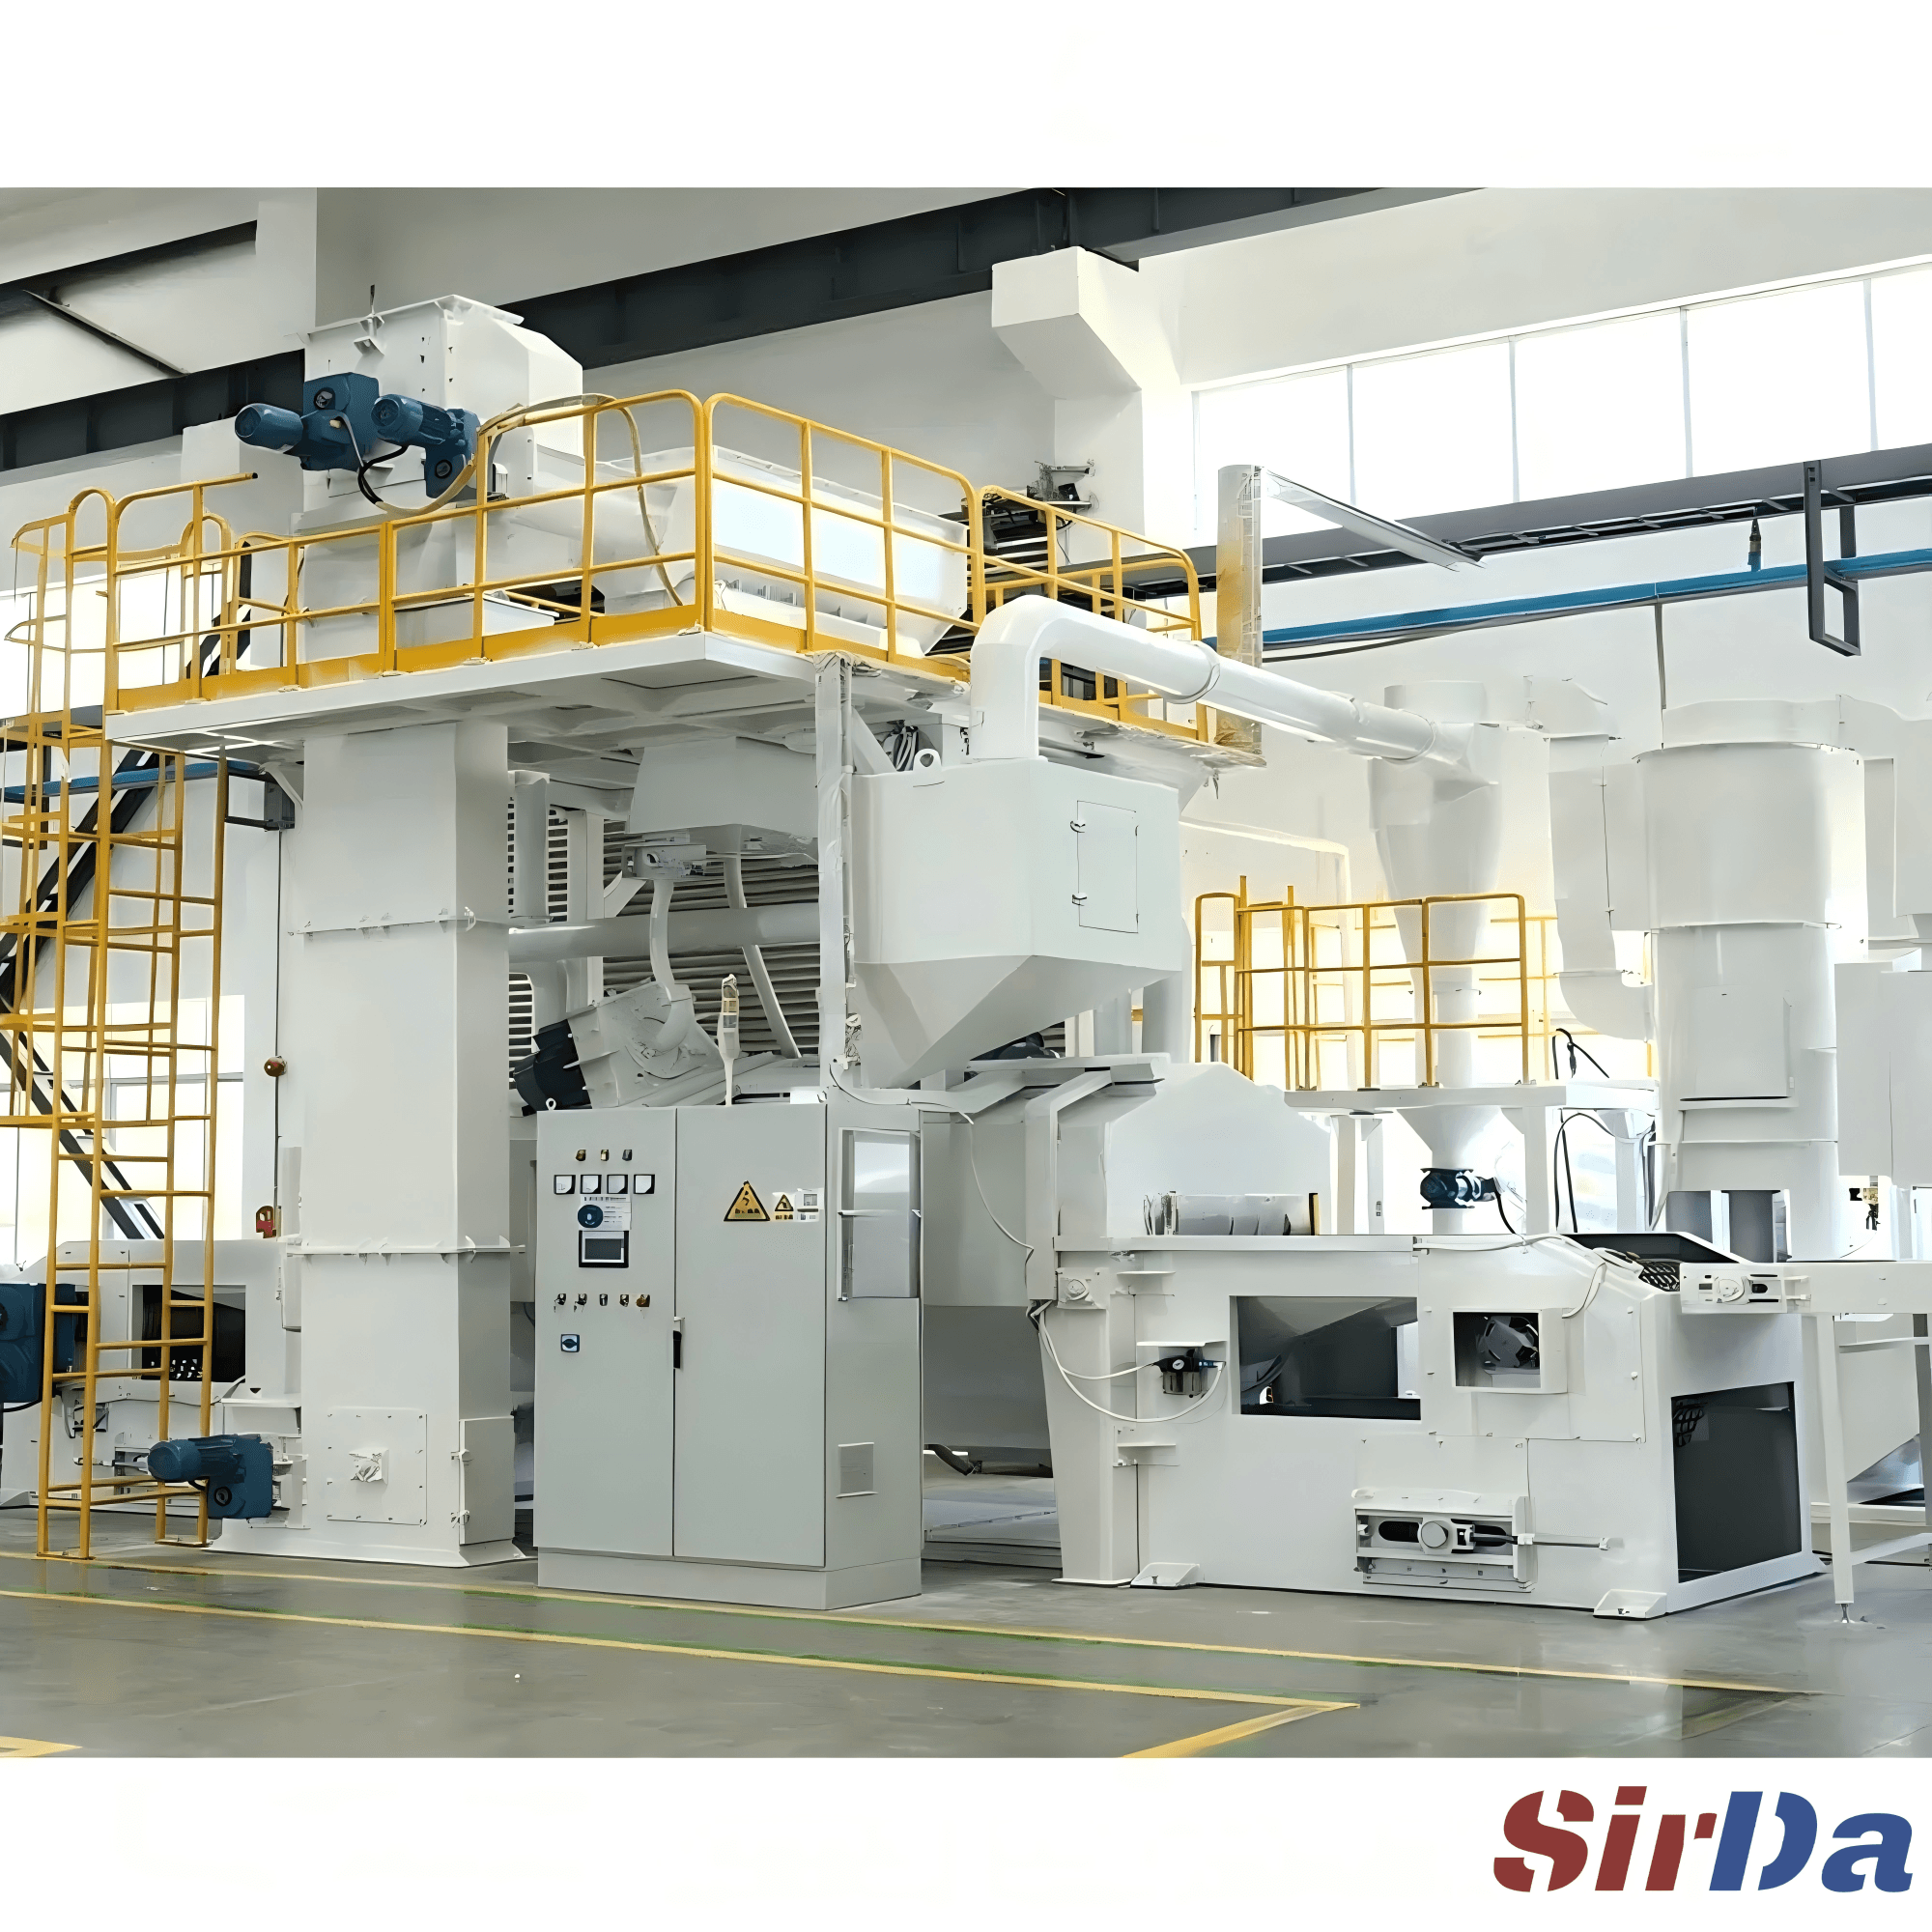
Project facts
- Industry
- Automotive components
- Country / region
- South America
- Workpiece
- Brackets, stampings and suspension parts, 0.2–3 kg
- Machine
- QWD800 mesh belt shot blasting machine
- Result / takt time
- 2.4 t/h continuous pass; SA 2.5 before e-coating

Your next project
Let’s find your solution.
Send your workpiece and production requirements.
Let’s define the right blasting system.